Multilayer PCBs are widely used in advanced electronics because they can integrate more circuits into a limited space while supporting complex electrical and mechanical requirements. However, achieving a reliable multilayer structure depends on much more than accurate circuit fabrication. The bonding process between cores, prepregs, and copper foils is equally important. This is where PCB Laminating Machines become essential.
A lamination system does not simply press several PCB layers together. It must create a carefully controlled combination of temperature, pressure, time, and often vacuum so that the resin flows correctly and the individual layers form a stable, uniform structure. IPC technical materials describe multilayer lamination as a process in which prepregs and cores are stacked and bonded under controlled heating, pressure, and, in many applications, vacuum conditions.
PCB Laminating Machines
What Are PCB Laminating Machines?
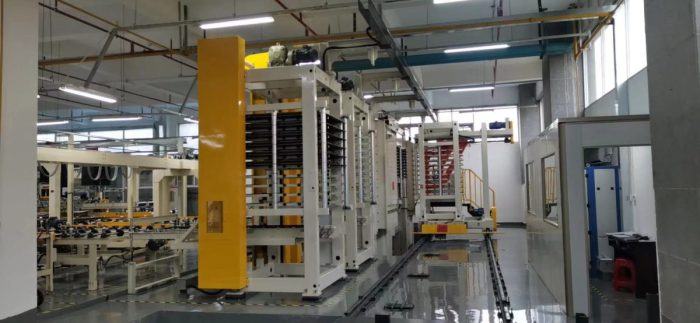
PCB Laminating Machines are industrial press systems designed to bond the different layers of a multilayer printed circuit board into one mechanically stable structure. A typical stack may include copper foils, inner-layer cores, and multiple prepreg sheets. During pressing, heat activates and cures the resin in the prepreg, while pressure promotes intimate contact between the layers.
Modern lamination equipment generally includes heated platens, pressure-control systems, temperature-monitoring systems, loading structures, and, depending on the application, vacuum capability. Multi-opening presses can process several stacks during one production cycle, improving manufacturing efficiency. The exact lamination profile depends on the resin system, prepreg condition, board construction, and material requirements.
For this reason, the machine should be viewed as a process-control platform rather than simply a large hydraulic press. Its ability to maintain stable temperature distribution, uniform pressure, appropriate heating and cooling rates, and repeatable cycles directly affects the consistency of the finished PCB.
How PCB Laminating Machines Affect PCB Performance
The lamination stage has a direct relationship with board thickness, dimensional stability, interlayer bonding, dielectric structure, and long-term reliability. If temperature or pressure is poorly controlled, resin flow may become inconsistent. Excessive resin flow can change the intended dielectric thickness, while insufficient flow may leave areas with poor bonding or internal voids.
Vacuum is particularly important for applications where trapped air or moisture could become a reliability concern. IPC notes that a low-temperature vacuum step may be introduced during lamination to reduce internal voids, which can otherwise provide locations for moisture entrapment.
The thermal cycle also matters. Different PCB materials require different processing windows, so a universal temperature-and-pressure recipe is not appropriate for every board. For example, high-frequency or high-temperature materials can require specialized lamination profiles. Rogers processing guidance for certain multilayer materials specifies controlled temperature, pressure, dwell time, and cooling conditions, illustrating why the process must be matched to the material system.
In practical manufacturing, good lamination quality can therefore contribute to better dimensional consistency, stronger interlayer bonding, stable dielectric properties, and improved resistance to thermal and mechanical stresses. Poor lamination, by contrast, can become the starting point for delamination, blistering, warpage, thickness variation, and reliability failures.
What Are the Cost Factors of PCB Laminating Machines?
The purchase price of a lamination press is only one part of the total cost. Machine capacity, platen size, number of openings, heating method, pressure range, vacuum capability, automation level, temperature-control accuracy, maintenance requirements, and energy consumption can all affect the investment.
For high-volume PCB manufacturers, production efficiency is particularly important. A machine capable of processing multiple stacks in one cycle can improve throughput, but higher capacity generally requires a larger initial investment. Advanced monitoring and automation can also increase equipment costs while reducing operator dependency and improving process repeatability.
Operating costs should also be considered. Energy consumption during heating and cooling, maintenance of hydraulic and vacuum systems, replacement of consumable or pressure-distribution materials, and downtime caused by equipment maintenance can significantly influence the long-term cost per panel. Reusable high-performance press pads, for example, are designed to withstand repeated lamination cycles and can reduce waste and running costs compared with disposable pressure-distribution materials.
From a manufacturer’s perspective, the most economical machine is not necessarily the one with the lowest purchase price. The better question is whether the equipment can consistently produce the required quality at the required production volume. A lower-cost press that generates frequent defects, long cycle times, or unstable results can ultimately be more expensive.
What Problems Can PCB Laminating Machines Cause?
Even when the basic equipment is correctly selected, lamination problems can occur if the machine, materials, and process parameters are not properly matched.
Delamination is one of the most serious concerns. It may result from insufficient bonding, contamination, excessive moisture, inappropriate curing conditions, or an unsuitable lamination cycle. Moisture control is particularly important because PCB materials can absorb moisture, which may contribute to degradation during manufacturing and later thermal exposure.
Voids and bubbles are another common concern. Entrapped air, moisture, or improper resin flow can create internal defects. Vacuum assistance and carefully controlled pressure and temperature profiles can help reduce this risk.
Warpage and dimensional distortion may occur when the thermal and mechanical stresses within the multilayer structure are not sufficiently controlled. Different materials have different coefficients of thermal expansion, so heating and cooling conditions can influence the final board shape. IPC research also identifies process-induced distortion as an important consideration in multilayer laminate processing.
Uneven thickness or resin distribution can result from incorrect pressure distribution, unsuitable prepreg selection, inconsistent material thickness, or poor press-pad conditions. These problems can eventually affect impedance, mechanical dimensions, drilling accuracy, and assembly performance.
The solution is not simply to increase temperature or pressure. Manufacturers should establish qualified lamination recipes for each material and stack-up, maintain accurate temperature and pressure calibration, control material storage conditions, inspect press surfaces and pads regularly, and monitor production results through appropriate quality-control procedures.
How to Improve PCB Laminating Machines and Process Control
Effective lamination quality control starts before the stack enters the press. Prepreg and core materials should be stored and handled according to their requirements, while stack-up design, copper distribution, prepreg thickness, and resin content should be reviewed before production.
During pressing, manufacturers should monitor temperature at relevant points rather than relying only on the nominal platen setting. Pressure should be applied according to the qualified process profile, while heating and cooling rates should remain within the limits appropriate for the material system.
Vacuum control can also be valuable for reducing trapped air and improving bonding consistency. After lamination, manufacturers can verify thickness, flatness, bonding quality, and other relevant characteristics through inspection and testing.
In my view, the biggest mistake is treating lamination as a single machine parameter. Temperature, pressure, vacuum, material condition, stack-up design, and cooling behavior interact with each other. A high-end press cannot compensate for poor material control, and excellent materials cannot fully compensate for an unstable process. The real objective should be to build a repeatable process window in which equipment, materials, and production parameters work together.
Types of PCB Laminating Machines
Laminating machines are classified according to their heating methods. The most common types include:
1. Electric Heater Laminating Press
These machines utilize electric heating elements, typically resistance wires, to generate heat, which is transferred to the laminating plates. The design is simple, and the cost is relatively low, making it a good option for manufacturers with budget constraints.
Pros:
-
Affordable: Simple technology leads to a lower cost for the equipment.
-
Ease of use: The machine is easy to operate and maintain.
Cons:
-
High energy consumption: Electric heating systems are generally more expensive than natural gas or diesel-powered alternatives.
-
Uneven heating: Over time, the resistance of the heating wires may change, leading to uneven heating, which negatively impacts lamination quality.
-
Slow heating: Heating times are longer compared to more advanced systems, which can slow down production.
-
Lower precision: For high-precision PCBs, this method does not provide the required accuracy.
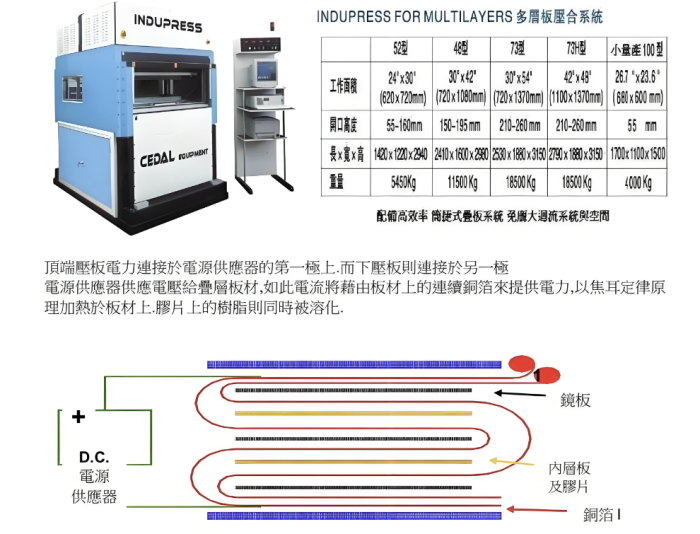
2. Copper Foil Heating Laminating Press
Copper foil heating presses utilize copper foil as the heat source, exploiting copper’s excellent thermal conductivity to distribute heat evenly across the laminating plate.
Pros:
-
Even heating: Copper’s high conductivity ensures uniform heat distribution, preventing hot spots.
-
Faster heating: This system is more efficient than electric heating, leading to shorter heating times.
-
Ideal for high-precision PCBs: This system is well-suited for applications requiring high precision and quality.
Cons:
-
Higher cost: Copper foil heating systems tend to be more expensive than electric systems.
-
Risk of fire: The system relies on temperature sensors, and poor placement or maintenance can lead to dangerous overheating and fires.
-
Equipment strength issues: Copper foil systems typically use black-oxide aluminum plates, which are not as durable as steel, leading to potential deformation and pressure issues during lamination.
-
Maintenance demands: Copper foil systems require frequent maintenance to ensure reliable operation.
Note: While this type of machine is commonly associated with Cedal laminating presses, it suffers from several significant issues, leading to limited adoption by many PCB manufacturers.
PCB Laminating Machines
3. Thermal Oil Heating Laminating Press
Thermal oil heating presses use thermal oil as the medium for heat transfer. This method provides consistent and even heating, operating at relatively low temperatures.
Pros:
-
Precise temperature control: Thermal oil systems offer precise temperature management, with individual plates maintaining temperature variation within ±1°C and across plates within ±2°C.
-
Energy savings: The thermal oil heating method is more energy-efficient than electric systems, saving 30%-50% in energy costs, depending on usage frequency.
-
Strong mechanical design: The use of steel plates and load-bearing decks provides strong mechanical stability and reduces PCB deformation.
Cons:
-
High initial cost: The investment required for thermal oil systems is higher than for other heating methods, and maintenance can also be costly.
-
Complex operation: This method requires careful temperature and pressure management to ensure uniform heating.
-
Energy consumption: Continuous heating is needed, which may result in higher energy use if the system is not frequently used.
Common Lamination Defects
Improper control during lamination can result in the following defects:
-
Layer delamination: Insufficient heating or pressure can cause layers to separate.
-
Bubbles: Air trapped during lamination can form bubbles between layers.
-
Uneven lamination: Inconsistent heating or pressure may cause uneven bonding, leading to surface deformations.
-
Copper foil detachment: Excessive temperature or pressure can cause copper foil to detach from the substrate.
SQPCB utilizes advanced thermal oil heating laminating presses along with high-precision temperature control systems to ensure that every PCB undergoes optimal lamination conditions. By strictly controlling temperature, pressure, and time, we ensure that each PCB meets international quality standards. This approach is especially well-suited for multi-layer PCBs and HDI boards.
Why PCB Laminating Machines Matter in Modern PCB Manufacturing
As PCB designs become thinner, denser, and more complex, the tolerance for manufacturing variation becomes smaller. Multilayer boards may contain many interfaces, fine geometries, controlled dielectric structures, and specialized materials. A small lamination problem that appears insignificant during fabrication can later become a serious electrical, mechanical, or reliability issue.
For PCB manufacturers, investing in capable equipment is therefore only the beginning. The greater value comes from combining reliable machinery with disciplined process engineering, material management, preventive maintenance, and quality inspection.
A well-controlled lamination process helps manufacturers reduce avoidable defects, improve production consistency, and maintain the structural integrity required by demanding applications. This is especially important when customers expect stable board thickness, accurate layer registration, reliable interlayer bonding, and consistent performance across production batches.
Ultimately, successful multilayer PCB manufacturing is not about using the most expensive press. It is about using equipment that matches the board structure and material system, then controlling the entire process with sufficient precision. When equipment capability and process discipline are aligned, lamination becomes a controlled manufacturing advantage rather than a hidden source of quality risk.
FAQs
1. What is the main function of PCB Laminating Machines?
Their primary function is to bond PCB cores, prepregs, and copper foils into a unified multilayer structure through controlled heat, pressure, time, and, when required, vacuum.
2. Why is vacuum used during PCB lamination?
Vacuum can help remove trapped air and reduce internal voids. This can improve bonding consistency and reduce locations where moisture may become trapped inside the multilayer structure.
3. How does lamination affect PCB performance?
Lamination can influence interlayer bonding, dielectric thickness, dimensional stability, mechanical strength, and long-term reliability. An unstable lamination process may contribute to defects such as delamination, voids, warpage, and thickness variation.
4. What are the major cost factors when selecting lamination equipment?
Important factors include equipment capacity, platen size, number of openings, temperature and pressure control, vacuum capability, automation, energy consumption, maintenance, consumables, and expected production volume.
5. How can PCB manufacturers reduce lamination defects?
Manufacturers can reduce defects by controlling material storage and moisture, using qualified stack-up and lamination recipes, calibrating temperature and pressure systems, maintaining vacuum equipment, inspecting press pads and surfaces, and monitoring finished-board quality.

- Special PCB
- long board pcb
- Flexible PCBs
- Special PCB
- Express Printed Circuit Board
- Pcb Prototype
- LED PCB
- PCB
- Pcb Meaning
- Printed Circuit Board
- Pcb manufacturer
- Rigid pcb board
 Quote
 E-mail